When buying a laser cutting machine, it is easy to focus on the maximum cutting speed listed by the manufacturer. You may see specifications such as 40 m/min, 60 m/min, or even 100 m/min and expect your machine to maintain that speed during production. However, the actual laser cutting speed can be much lower depending on the material, thickness, laser power, cutting parameters, and part geometry.
This does not necessarily mean the machine is underperforming. Maximum speed and actual production speed are two different things. Understanding the factors that affect laser cutting speed can help you evaluate machine performance more realistically and avoid choosing equipment based only on a specification sheet.
Maximum Cutting Speed vs. Actual Production Speed
The maximum speed of a laser cutting machine usually represents the highest movement speed under specific conditions. It does not mean the machine can cut every material and thickness at that speed.
For example, a machine may be capable of moving at 100 m/min when cutting an empty path or a simple thin sheet. Cutting a thick carbon steel plate with multiple holes and corners is completely different.
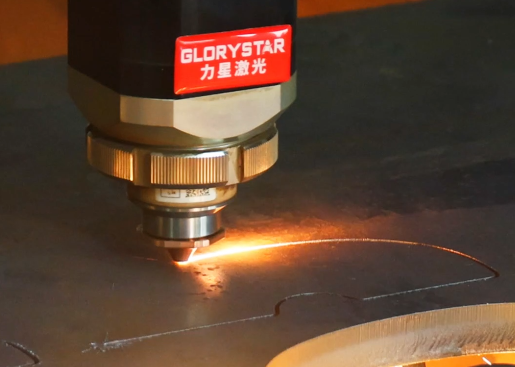
During real production, the machine may need to slow down for piercing, corners, small holes, curves, and changes in direction. Therefore, the effective production speed depends not only on the machine's maximum speed but also on the entire cutting process.
1. Material and Thickness Affect Laser Cutting Speed
Different metals require different cutting conditions.
Carbon steel, stainless steel, aluminum, brass, and copper have different thermal and reflective properties, so they cannot always be processed at the same speed.
Thickness is equally important. Thin sheet metal can generally be processed faster than thick plate because the laser needs to remove less material.
For this reason, when comparing machines, it is more useful to ask for laser cutting speed by material and thickness instead of looking only at the maximum speed.
2. Laser Power Matters, But More Power Does Not Solve Everything
Laser power has a direct impact on cutting capability. Higher power can provide more energy to the material, making it possible to process thicker metal or increase cutting speed within a suitable thickness range.
However, doubling the laser power does not automatically double the production speed.
The optimal laser cutting speed depends on the relationship between laser power, material, thickness, focus position, assist gas, and other cutting parameters.
A higher-power machine is most valuable when your production requires frequent processing of thicker materials or higher throughput.
3. Assist Gas Can Change Cutting Performance
Assist gas plays an important role in the cutting process.
Oxygen, nitrogen, and compressed air can produce different results depending on the material and application. Gas pressure, purity, and flow also affect the cutting process.
If the gas supply is insufficient or the parameters are not properly matched to the material, operators may need to reduce the cutting speed to maintain edge quality and cutting stability.
This is why gas consumption and gas requirements should also be considered when evaluating the overall performance of a laser cutting machine.
4. Focus Position and Cutting Parameters Matter
Even when a machine has sufficient laser power, incorrect parameters can prevent it from achieving the expected speed.
Focus position, laser power, cutting speed, frequency, duty cycle, nozzle selection, and other settings all work together.
If the focus is incorrect or the parameters are too aggressive, the machine may produce excessive dross, rough edges, incomplete cuts, or unstable piercing. Operators then have to reduce the speed to maintain quality.
In practical production, the fastest setting is not always the best setting. A slightly lower speed that produces consistent parts may deliver better overall productivity.
5. Part Geometry Can Reduce Average Speed
A machine may cut a long straight line very quickly, but real parts rarely consist only of straight lines.
Small holes, sharp corners, curves, short line segments, and complex contours require the cutting head to change direction and speed.
For example, a cutting head cannot approach a sharp corner at maximum speed and immediately change direction without affecting accuracy or edge quality. The machine therefore reduces speed before and after the corner.
This means two parts made from the same sheet can have very different processing times.
6. Acceleration and Deceleration Also Matter
Maximum speed is only one part of machine motion performance.
The cutting head must constantly accelerate and decelerate as it moves between different sections of a part. On small or complex components, the machine may spend more time changing speed and direction than actually moving at its maximum speed.
This is particularly important when comparing high-speed laser cutting machines. A machine with a high advertised maximum speed is not necessarily the fastest machine in real production.
Acceleration performance, motion control, machine rigidity, and cutting head response can all affect the final cycle time.
7. Piercing Time Can Have a Major Impact
For thicker materials, piercing can become a significant part of the total processing time.
If a sheet contains hundreds of holes, the machine may spend considerable time piercing before it starts cutting each contour.
As a result, increasing the cutting speed alone may not significantly reduce the total production time.
For high-volume production, it is therefore important to evaluate both cutting speed and piercing performance.
Why Parts per Hour Matter More Than Maximum Speed
For most manufacturers, the real goal is not to achieve the highest number on a specification sheet. The goal is to produce more finished parts in less time.
A better way to evaluate a machine is to look at:
Total cycle time per part
Parts produced per hour
Material utilization
Piercing time
Cutting quality
Machine uptime
Operator involvement
For example, a machine that cuts at a slightly lower speed but completes a part faster because of better acceleration, piercing, nesting, and automation may deliver higher actual productivity.
How to Evaluate Laser Cutting Speed Before Buying
Before purchasing a laser cutting machine, provide the manufacturer with your actual production requirements.
Share the materials and thicknesses you process most frequently, typical part drawings, required tolerances, and expected production volume. A sample test can then provide a more realistic picture of the machine's performance.
Instead of asking only, “What is the maximum cutting speed?”, ask:
“How long will it take to produce my actual parts?”
This approach gives you a much clearer understanding of the machine's real production capability.
Final Thoughts
The actual laser cutting speed of a machine is influenced by far more than its maximum rated speed. Material, thickness, laser power, assist gas, focus position, cutting parameters, part geometry, acceleration, and piercing time can all affect the final production cycle.
When comparing laser cutting machines, look beyond the highest speed listed in the specifications. The more important question is whether the machine can consistently produce your parts at the required quality, cost, and production volume.
For manufacturers evaluating new equipment, testing your own materials and parts before making a purchase can be one of the most reliable ways to determine the right laser cutting solution.